The short answer
A bridge saw is normally the direct, productive choice for slab sizing, straight cuts, repeated rectangles, polygons and many 45° operations. A waterjet is the stronger choice for internal openings, small-radius corners, curves, floor inlays and other CAD-defined shapes a circular blade cannot reach.
Ask which machine can produce the required geometry, with an acceptable edge, at the volume your factory needs.
Side-by-side comparison
| Decision | Bridge saw | Abrasive waterjet |
|---|---|---|
| Typical work | Slab sizing, straight cuts, rectangles, polygons and mitres | Holes, internal cut-outs, curves, lettering, inlays and intricate profiles |
| Tool geometry | Rotating blade needs entry, exit and turning space | Narrow cutting stream follows CAD paths and reaches internal geometry |
| Heat effect | Low when correctly cooled, but uses mechanical blade contact | Cold cutting without a conventional heat-affected zone |
| Important quality checks | Chipping, corner breakage, squareness, blade marks and dimension | Kerf, taper, pierce quality, striation, small-part movement and dimension |
| Programming | Simple dimensions through CNC or machine interface; some models include imaging/layout | CAD/CAM file preparation, path order, lead-ins, nesting and kerf compensation |
| Consumable focus | Blade condition, dressing, cooling and feed settings | Abrasive, orifice/nozzle, seals, filters, high-pressure components and water quality |
| Best production role | Efficient primary sizing and repeat geometric cutting | Flexible secondary cutting or specialty-shape production |
Choose a bridge saw when repeat geometry dominates
If most orders begin with full slabs and become rectangular countertop blanks, steps, wall panels or other straight-sided parts, a bridge saw usually owns the first cutting stage. The blade is easy for operators to understand, the process is direct, and the machine can be matched to loading, layout and 45° cutting requirements.
Check these points before purchase
- Maximum usable cutting length and width, not only nominal table size
- Blade diameter and material-specific blade package
- Head rotation and 45° capability for the required slab thickness
- Imaging, nesting or vacuum handling functions, if included
- Edge-quality test using the customer’s slab and typical cut sequence
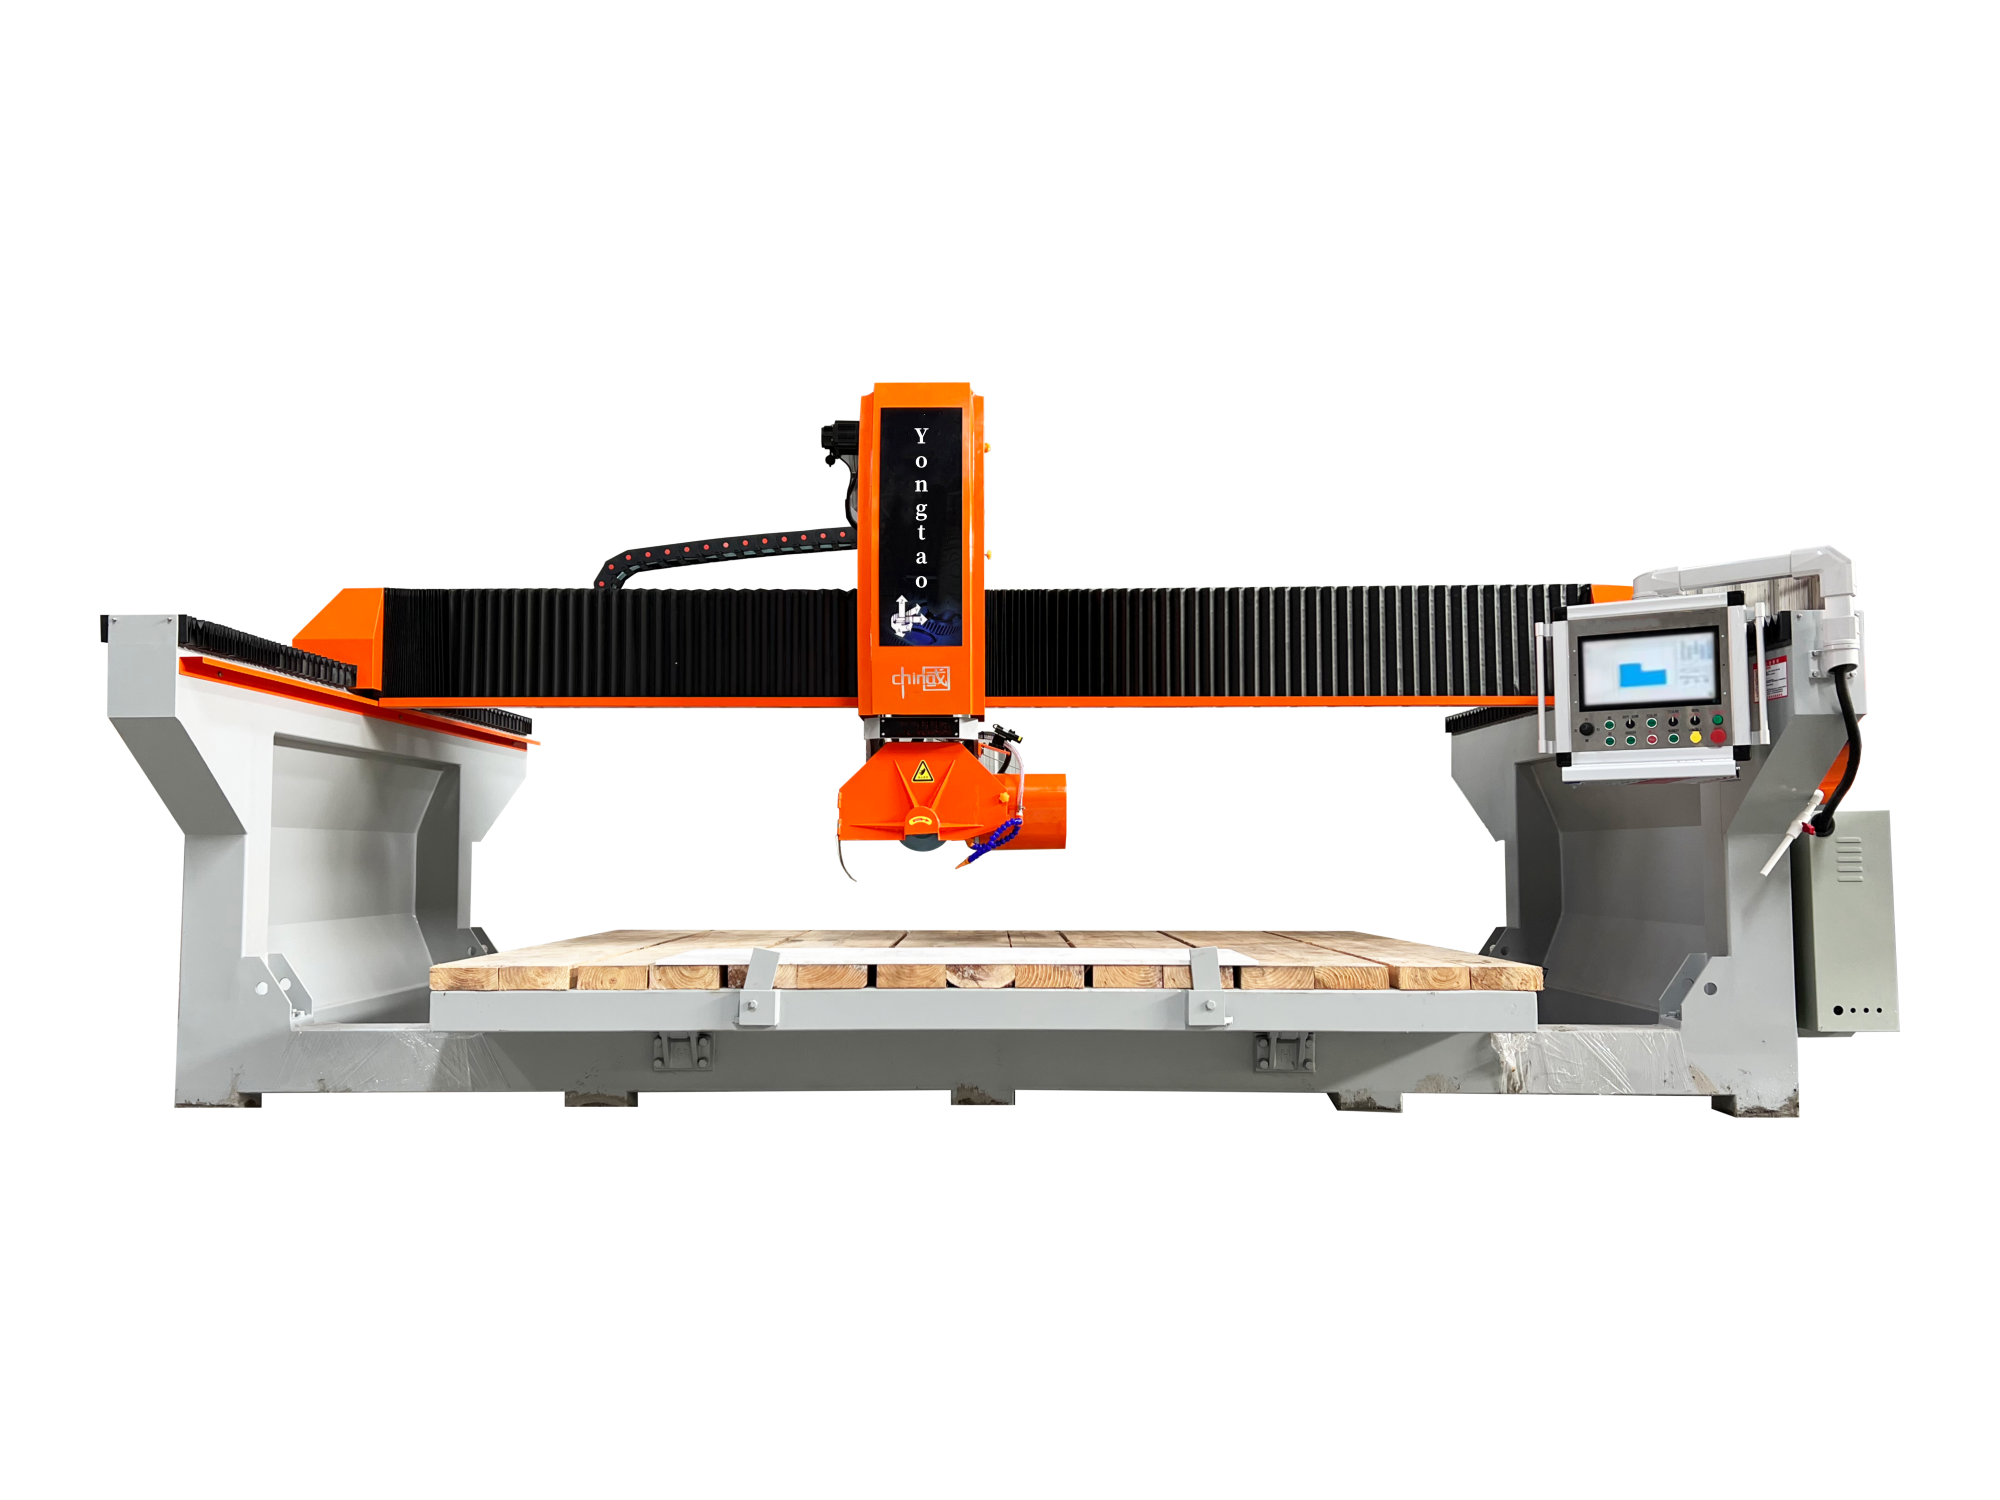
A bridge saw is less comfortable with internal openings and tight concave shapes. Operators may need overcuts, drilling, secondary manual work or another machine for these features.
Choose a waterjet when geometry drives the job
A waterjet follows a programmed path with a narrow abrasive stream. This makes it suitable for sink and tap openings, curved countertop parts, medallions, mosaics, lettering and profiles with internal corners.
The machine is only half of the waterjet process
Good results also depend on CAD preparation, lead-in position, piercing method, cutting direction, kerf compensation, abrasive flow, material support and small-part retention. A sample test should reproduce these conditions, not just cut a simple square.
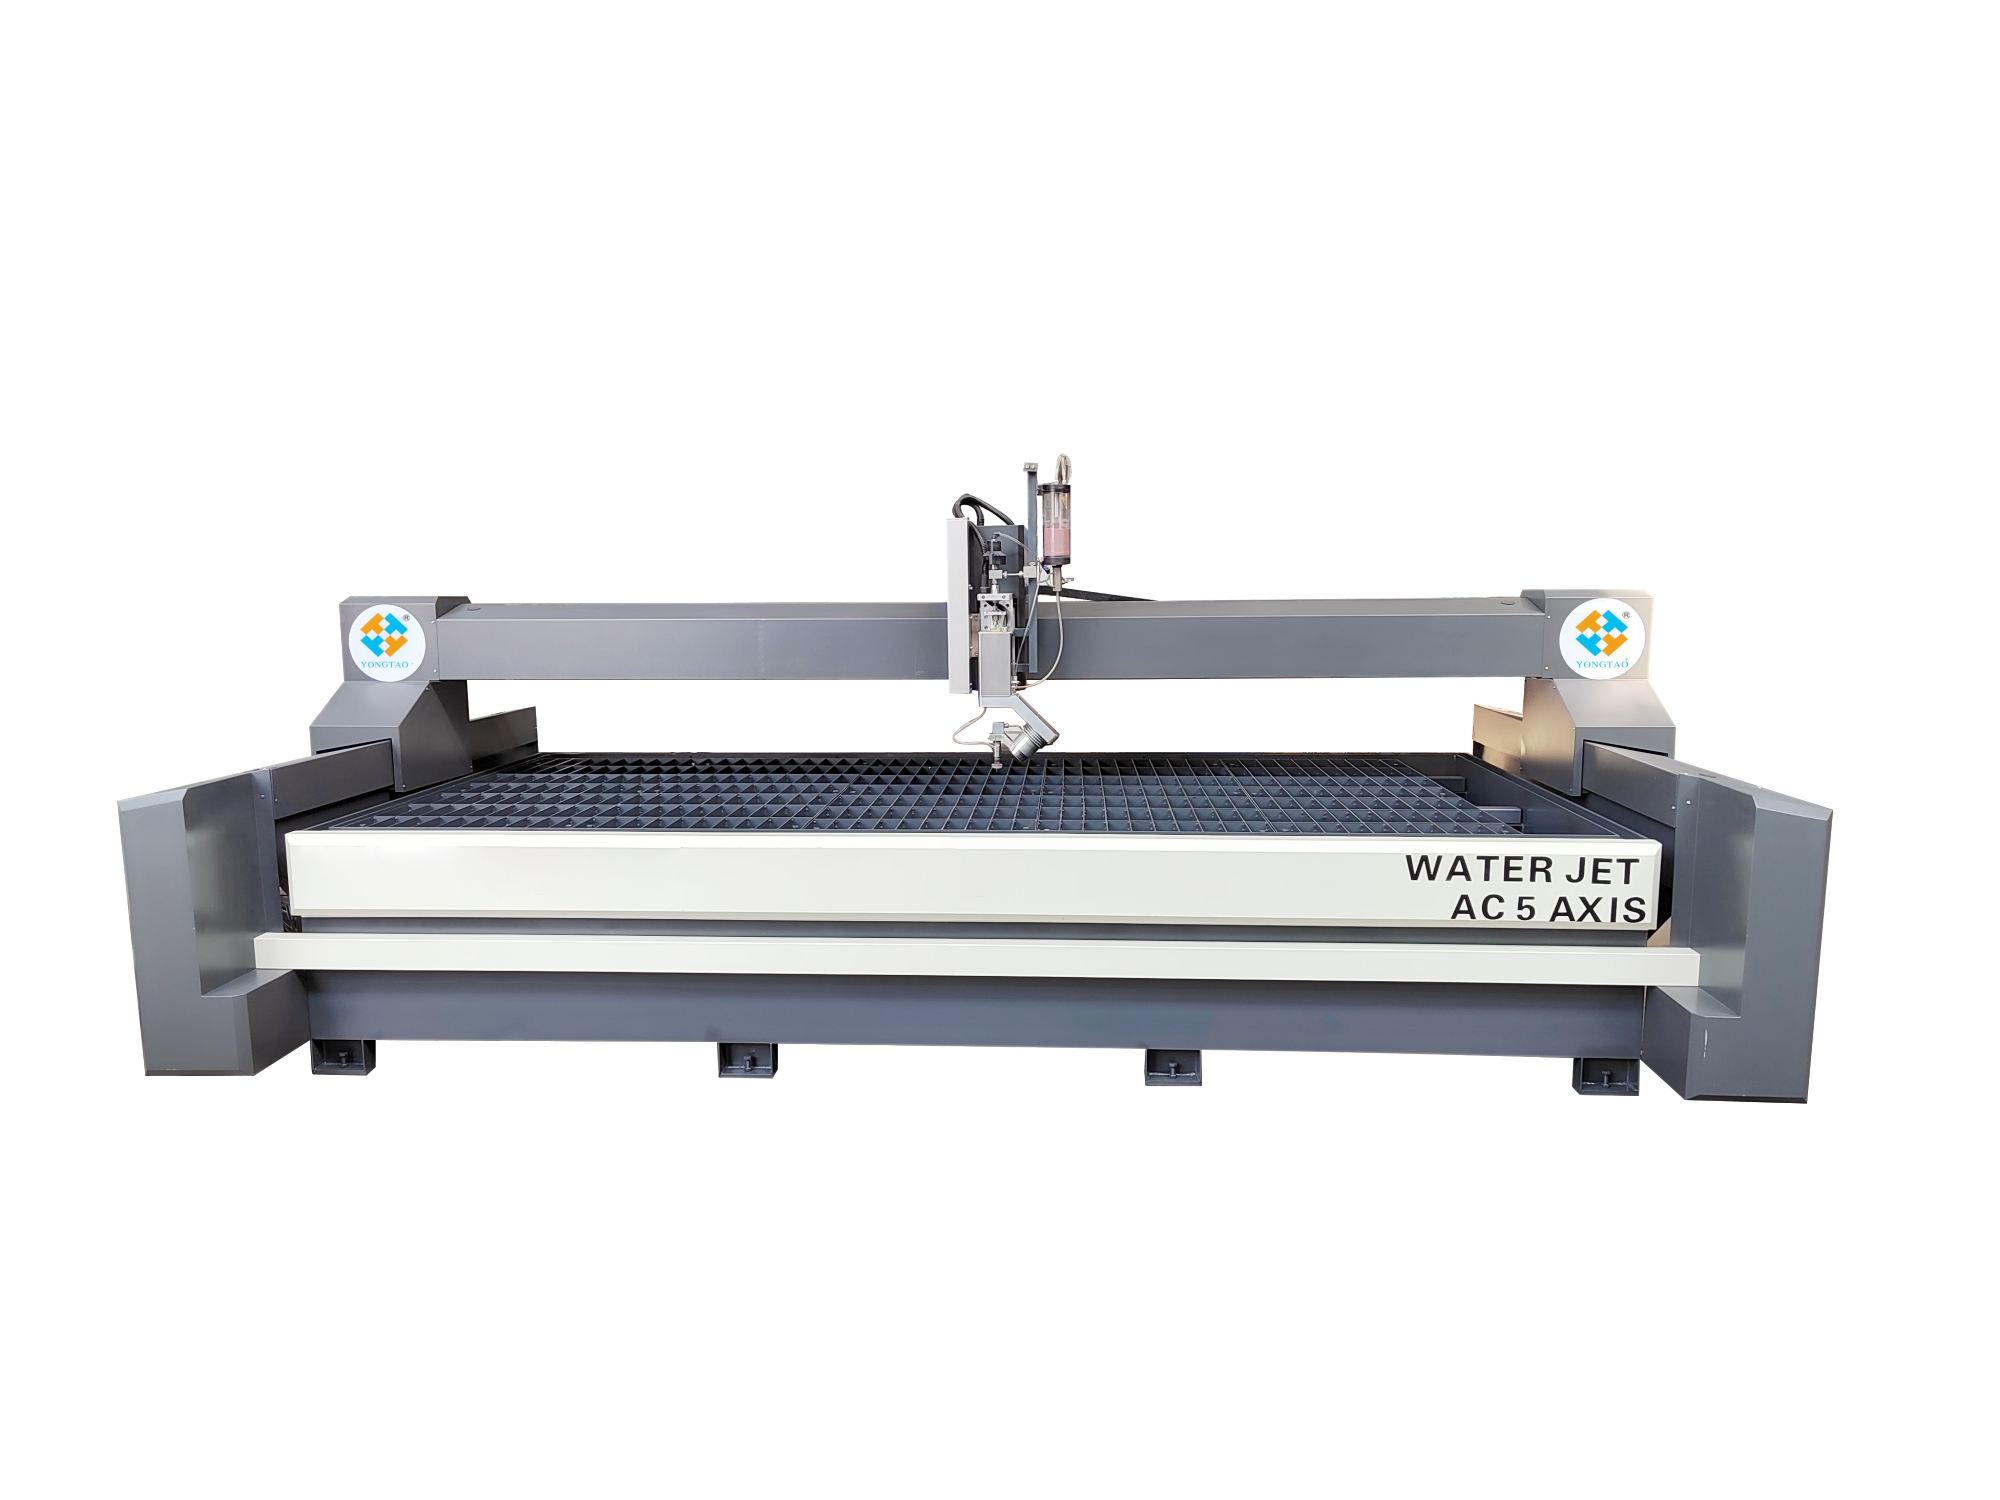
Waterjet operating cost includes high-pressure wear parts and abrasive consumption. Those costs may be justified for shapes that would otherwise require manual work, multiple machines or unacceptable compromises.
Many countertop factories need both
A practical mixed line can use the bridge saw for primary sizing and repeat geometric cuts, then route parts requiring sink openings, curves or special profiles to the waterjet. This keeps straightforward work on the simpler process while preserving flexibility for complex orders.
A typical division of work
- Image or measure the slab and plan the primary layout.
- Use the bridge saw for the main straight cuts and rectangular components.
- Move selected parts to the waterjet for internal openings and complex contours.
- Complete edge profiling, chamfering or polishing.
- Dry fit and inspect before packing or installation.
Send this information for a useful recommendation
- Material names, slab sizes and thickness range
- Representative DXF drawings or clear finished-product photos
- Percentage of straight cuts versus holes, curves and complex shapes
- Required pieces per shift and current operator count
- Edge-quality, dimension and taper acceptance requirements
- Factory space, voltage, water conditions and waste-treatment plan
With these inputs, Yongtao can recommend whether one machine is sufficient, which process should come first and what sample test will prove the decision.